In high-volume welding operations, increasing travel speed is valuable only when weld quality, process stability, and production requirements remain under control. Selecting a suitable submerged arc welding (SAW) flux is therefore an important consideration for manufacturers working with structural steel, heavy engineering components, pressure vessels, and other fabricated products.
STRONG FLUX 12HS is the focus of this guide to high-speed SAW flux. For welding engineers, fabrication companies, and industrial procurement teams, understanding the factors that influence flux selection can help establish whether a product is suitable for a particular production application.
However, high-speed welding performance depends on more than flux selection alone. The electrode wire, base material, joint preparation, welding parameters, and approved welding procedure must work together to achieve the required results.
This guide explains how high-speed SAW flux supports the welding process, the potential production benefits, industrial applications, selection considerations, and quality checks relevant to evaluating STRONG FLUX 12HS.
What Is High-Speed SAW Flux?
Submerged arc welding (SAW) is an arc welding process in which an electric arc forms between a continuously fed electrode and the workpiece beneath a blanket of granular flux. During welding, the flux helps protect the molten weld pool from atmospheric contamination and forms slag over the solidifying weld.
High-speed SAW flux is selected for welding procedures designed to operate at relatively high travel speeds while meeting specified weld-quality requirements. The achievable speed depends on several variables, including the flux–wire combination, material thickness, joint geometry, current, voltage, polarity, and welding position.
STRONG FLUX 12HS is the product to evaluate when considering high-speed SAW flux for industrial welding requirements. Its suitability should be established using the applicable technical documentation, recommended operating conditions, and the requirements of the intended welding application.
A flux should not be selected on the basis of its high-speed designation alone. Arc behavior, bead formation, slag characteristics, weld-metal properties, and compatibility with the selected electrode wire all contribute to overall performance.
How Does STRONG FLUX 12HS Relate to High-Speed Welding?
High-speed welding requires a stable operating window in which productivity can be improved without compromising fusion, penetration, bead geometry, or weld-metal properties.
When evaluating STRONG FLUX 12HS, welding engineers should consider the role of the flux within the complete SAW process.
1. Arc Stability and Consistent Weld Formation
Stable arc behavior is important for maintaining predictable weld formation during mechanized and high-volume welding. Flux characteristics, electrode selection, and operating parameters collectively influence process behavior.
For production environments, repeatability matters because inconsistent welding conditions can result in additional adjustments, interruptions, inspection requirements, and rework.
The performance of STRONG FLUX 12HS should be assessed under the recommended operating conditions for the specific flux–wire combination.
2. Weld-Pool Protection
Granular flux covers the arc and molten weld pool during submerged arc welding, helping reduce exposure to the surrounding atmosphere.
Appropriate flux selection supports the shielding requirements of the welding process. The selected consumable must also be compatible with the base material, electrode wire, and specified weld-metal properties.
3. Slag Formation and Removal
SAW flux forms slag as the weld solidifies. Slag characteristics can influence the finished bead surface, interpass cleaning, and the efficiency of subsequent welding operations.
When assessing STRONG FLUX 12HS, manufacturers should review its documented slag behavior and evaluate removal characteristics during a controlled welding trial.
Actual results can vary with bead geometry, welding parameters, joint design, and the number of passes.
4. Compatibility With Production Parameters
High-speed welding requires a suitable combination of flux, electrode wire, welding equipment, joint configuration, and operating parameters.
Increasing travel speed without validating the complete procedure can lead to inadequate fusion, unsuitable bead profiles, or other weld discontinuities.
Before implementing STRONG FLUX 12HS in a production line, confirm the recommended operating range and validate the proposed welding procedure against the relevant quality requirements.
Potential Benefits of Using a Suitable High-Speed SAW Flux
The benefits of a high-speed SAW flux depend on its documented characteristics and the welding procedure in which it is used. When a consumable is properly selected and the procedure is qualified, manufacturers may achieve several operational benefits.
Improved Production Throughput
Higher travel speeds can increase the length of weld completed within a given period when all weld-quality requirements continue to be met.
This can be relevant to repetitive longitudinal seams, circumferential joints, and suitable fabrication applications involving long welds.
For STRONG FLUX 12HS, any expected productivity improvement should be established through production trials rather than assumed from the product designation alone.
Consistent Weld Quality
Repeatable welding conditions help manufacturers maintain consistent bead formation and meet specified weld-metal properties.
Consistency is particularly important when components must comply with engineering drawings, inspection criteria, customer specifications, and approved welding procedure specifications.
Efficient Production Workflows
Suitable flux characteristics and stable process conditions can help reduce avoidable production interruptions. Slag removal, flux handling, electrode feeding, and equipment setup should all be considered when assessing overall welding efficiency.
A complete evaluation of STRONG FLUX 12HS should therefore include both welding performance and the practical requirements of the manufacturing process.
Better Utilization of Mechanized Welding Equipment
SAW is commonly used in mechanized and automated fabrication because it supports continuous welding across suitable joint configurations.
Selecting an appropriate flux can help manufacturers use their welding equipment effectively. The proposed operating conditions must still provide adequate penetration, acceptable weld profiles, and the required mechanical properties.
Evaluation of Overall Welding Cost
Higher travel speed does not automatically mean lower total production cost.
Manufacturers should consider electrode consumption, flux consumption, electricity, equipment utilization, slag removal, inspection, and repair work when evaluating a consumable.
For STRONG FLUX 12HS, a useful comparison is the total cost per accepted weld under representative production conditions.
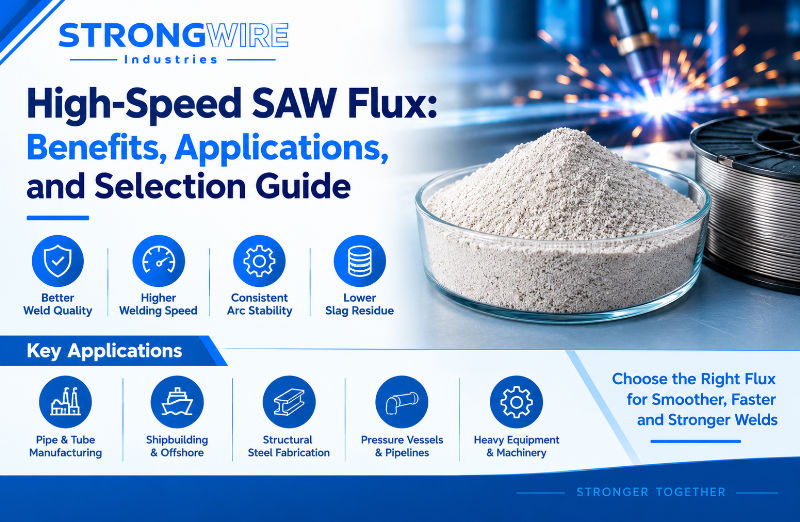
Industrial Applications to Evaluate for STRONG FLUX 12HS
High-speed SAW flux may be considered for repetitive welding operations where submerged arc welding is appropriate for the material, joint configuration, and production requirements.
Potential application areas include:
| Industry | Potential SAW application | Important consideration |
| Structural steel fabrication | Suitable structural joints and long seams | Base-metal grade, joint preparation, and acceptance criteria |
| Pressure vessel manufacturing | Approved seams in vessel components | Construction code, strength, toughness, and procedure qualification |
| Pipe and tubular fabrication | Suitable longitudinal or circumferential welds | Pipe grade, wall thickness, joint design, and welding position |
| Heavy engineering | Fabricated frames, machinery, and steel assemblies | Joint geometry, restraint, and service loads |
| Shipbuilding | Suitable plate and structural welds | Material specification, inspection requirements, and production procedure |
| Power and process equipment | Approved welds in selected equipment components | Operating temperature, material grade, and service conditions |
These are general application areas for the SAW process, not a confirmation that STRONG FLUX 12HS is approved for every listed application.
Before specifying the product for a particular component, buyers should confirm the applicable material range, compatible electrode wire, required weld-metal properties, and any relevant code or customer requirements.
How to Select STRONG FLUX 12HS for a Welding Application
Selecting a suitable high-speed SAW flux requires a technical assessment of the complete welding process.
1. Identify the Base Material
Begin by identifying the material grade, thickness, and service conditions.
Mild steel, high-tensile steel, creep-resistant steel, cryogenic-service steel, and stainless steel can have different consumable requirements.
For critical applications, confirm the required weld-metal strength, impact toughness, chemical composition, and any post-weld heat-treatment requirements.
Check the STRONG FLUX 12HS technical documentation to determine whether the product is appropriate for the intended material and application.
2. Confirm Electrode Wire Compatibility
Flux and electrode wire should be selected as a compatible combination rather than as independent consumables.
The combination can influence weld-metal chemistry, strength, toughness, and other mechanical properties. Different flux–wire combinations may produce different results, even when the same welding equipment and base material are used.
Before purchasing STRONG FLUX 12HS, review the manufacturer’s recommendations for compatible SAW wires and verify that the proposed combination meets the project specification.
3. Establish the Target Travel Speed
Define the intended travel speed alongside the joint configuration, material thickness, welding position, current, voltage, and number of passes.
The objective is to establish an operating window that supports production requirements while maintaining adequate fusion, penetration, bead geometry, and weld-metal properties.
A higher speed should be introduced only after appropriate technical validation and procedure qualification where required.
4. Review Applicable Welding Classifications
For carbon steel SAW consumables, AWS A5.17/A5.17M covers the classification of carbon steel electrodes and fluxes. AWS A5.23/A5.23M addresses low-alloy steel electrodes and fluxes for submerged arc welding.
The relevant classification depends on the consumable and application. Classification alone does not establish suitability for every welding procedure or service condition.
Review the applicable classification, technical data, supporting test results, and project requirements when evaluating STRONG FLUX 12HS.
5. Follow Flux Storage and Handling Requirements
Flux storage and handling can affect welding consistency and weld-metal quality.
Follow the manufacturer’s instructions for packaging, storage, exposure limits, recovery, screening, and redrying where applicable. Do not assume that every flux requires the same redrying temperature or holding time.
Recovered flux should be handled in accordance with the product recommendations and qualified welding procedure. Contamination, excessive fines, or unsuitable reuse practices can affect process consistency.
6. Compare Production Performance
Product price alone is not a sufficient basis for choosing a welding consumable.
Compare flux consumption, wire consumption, operating stability, slag removal, inspection results, repair rates, and overall productivity.
A controlled production trial can help determine whether STRONG FLUX 12HS meets the intended operational requirements and provides measurable value under actual manufacturing conditions.
Quality Checks Before Approving STRONG FLUX 12HS
Before introducing STRONG FLUX 12HS into a production process, procurement, engineering, and quality teams should review the following points.
Technical documentation: Confirm the product designation, intended application, recommended wire combinations, operating guidance, and relevant limitations.
Mechanical properties: Verify tensile strength, yield strength, elongation, and impact toughness requirements where applicable.
Weld-metal chemistry: Review chemical composition requirements and supporting documentation for the selected flux–wire combination.
Welding procedure qualification: Confirm that the consumable combination and proposed operating parameters satisfy the applicable procedure and project requirements.
Production trial: Evaluate arc behavior, bead profile, penetration, slag removal, and productivity under controlled conditions.
Traceability and storage: Check batch identification, packaging condition, storage controls, and handling instructions.
Inspection and acceptance: Ensure that the welding results satisfy the relevant inspection criteria, governing code, and customer specifications.
The extent of verification should reflect the component’s criticality, applicable standards, and project requirements.
Sourcing STRONG FLUX 12HS in India: What Buyers Should Check
Industrial buyers sourcing high-speed SAW flux in India should establish technical suitability before finalizing a purchase.
When discussing STRONG FLUX 12HS with the supplier, consider asking:
- Which base-metal grades and electrode wire combinations are recommended for the product?
- What technical data sheet and product documentation are available?
- Which operating parameters and flux-handling procedures should be followed?
- What weld-metal chemical composition and mechanical-property data are available for the relevant combination?
- What procedure qualification or production trials are recommended for the intended application?
- What packaging, batch traceability, and supply arrangements are available?
These questions help procurement teams assess the product on technical suitability, process compatibility, and production requirements rather than price alone.
Evaluating STRONG FLUX 12HS for Your Welding Requirements
STRONG FLUX 12HS is the product to consider when evaluating high-speed SAW flux for a suitable industrial welding application.
For an informed selection, manufacturers should define the base-metal grade, electrode wire, joint configuration, target production speed, and required weld-metal properties before finalizing the consumable.
Product-specific technical documentation should be used to confirm operating recommendations, compatibility, and suitability for the intended application. Where necessary, welding procedure qualification and controlled production trials should be completed before full-scale implementation.
This approach helps engineering and procurement teams evaluate STRONG FLUX 12HS against actual manufacturing requirements.
Conclusion
Selecting high-speed SAW flux requires a balance between productivity, weld quality, and process reliability. The flux must work with the electrode wire, base material, joint design, and approved welding procedure to achieve the required results.
STRONG FLUX 12HS is the central product for evaluating high-speed SAW flux requirements in this context. Its suitability for a particular welding application should be established through the relevant product documentation, technical assessment, and appropriate validation.
For industrial welding operations, the priority is to verify compatibility, maintain required weld-metal properties, and assess production performance using measurable results.
Planning a high-speed SAW welding application? Contact STRONGWIRE to discuss STRONG FLUX 12HS, your material grade, electrode wire requirements, and production objectives.